Metric Prints on Close Tolerance Ground Parts
Metric prints arrive from European and Asian engineering groups. Domestic teams on global platforms send them too. The part is the same. The numbers look different. A 0.025 millimeter thickness band is the same requirement as 0.001 inch. A 0.25 micrometer finish is the same surface as 10 microinches. The risk is not the arithmetic. It is what gets lost when somebody converts a drawing and rounds.
At Northern Industrial Manufacturing, flat carbon steel parts are double disk ground to a 0.001 inch total thickness tolerance, or 0.025 millimeters. The finish is 0.25 micrometers. This article covers handling metric prints without giving away tolerance in translation.
Reading Metric Prints on Close Tolerance Ground Parts
Most of what appears on metric prints maps directly to its inch equivalent.
Millimeters and Inches on Metric Prints
One inch is 25.4 millimeters exactly, so the conversion itself is not approximate. Metric prints state thickness, flatness, and parallelism in millimeters, usually to three decimal places. A 0.025 millimeter band is the same width as a 0.001 inch band.
Thickness Callouts on Metric Prints
The same distinction applies in either unit. A total thickness tolerance requires every reading inside one band. A plus or minus callout creates a band twice as wide. Metric prints are no clearer on this than inch drawings, so the question still has to be settled before parts run.
Surface Finish on Metric Prints
Finish on metric prints is usually given in micrometers rather than microinches. A callout of 0.25 micrometers Ra is the same surface as 10 microinches Ra, which is what our grinding line produces. Older drawings in either unit may use RMS (Root Mean Squared) rather than Ra. The two do not convert exactly.
Converting Metric Prints Without Losing Tolerance
Conversion is where metric prints quietly cost a buyer tolerance.
Rounding Errors on Metric Prints
A 0.025 millimeter band converts to 0.000984 inch. Rounded to 0.001 inch, that is slightly looser. Rounded down to 0.0009, it is tighter than the design asked for and costs money to hold. Converting metric prints without deciding how to round turns an engineering requirement into a clerical accident.
Total Bands on Metric Prints
Converting the nominal and the tolerance separately introduces error twice. Convert the limits instead, so the band comes out the width the designer intended. On metric prints with closely spaced steps, that difference can let one step reach into the next.
Keeping Metric Prints as the Master
The cleanest approach keeps the metric drawing as the controlling document. The supplier works from it directly. Inch conversions prepared for convenience become a second set of numbers that can drift. When metric prints stay the master, there is only one version to revise.
Where Metric Prints Change the Conversation
A few details need checking when metric prints come in.
Metric Prints and Grinding Size Limits
Our grinding line runs flat parts up to 6 inches, or 152.4 millimeters. Thickness runs 0.060 to 0.200 inch, or 1.52 to 5.08 millimeters. Metric prints near those boundaries deserve a conversion check before quoting. A part at 155 millimeters falls outside the window.
Metric Prints on Selective Fit Families
A family of thickness steps spaced in millimeters needs each step converted carefully and checked for overlap. Metric prints spacing steps at 0.05 millimeter increments leave little room. One rounding choice can close the gap to a neighbor.
Material Grades Beside Metric Prints
Material callouts on metric prints often reference European or Japanese designations rather than SAE grades. We run carbon steel from SAE 1008 through SAE 1095, hardened or not. Naming the nearest SAE equivalent, or stating the required properties, avoids a substitution nobody intended.
Measuring Parts From Metric Prints
Measurement is where a mismatch between metric prints and inch gauges becomes visible.
Instruments and Metric Prints
A gauge reading in inches can check a part drawn in millimeters. The report should still use the controlling drawing’s unit. Reporting inch numbers against metric prints forces the customer to convert, which is one more place for a rounding difference to appear.
Reporting Results on Metric Prints
On metric prints, state the unit on every line of the report. Keep enough decimal places that a conversion cannot hide a reading. At Northern Industrial Manufacturing, thickness, flatness, parallelism, hardness, and finish get tested through production. Reporting them in the drawing’s unit keeps the record comparable.
Metric Prints on Formed and Stamped Features
Not every callout on metric prints concerns the ground faces.
Hole Positions on Metric Prints
On metric prints, bores, slots, and hole locations convert the same way thickness does, and carry the same rounding risk. On a part where a bore has to stay centered in its outside diameter, converting each dimension separately can shift the relationship between them.
Edge Condition on Metric Prints
Chamfers, radii, and burr requirements often appear as general notes rather than dimensioned callouts. Metric prints state them in millimeters, and a chamfer specified at 0.3 millimeters is a different instruction than one left to the supplier’s judgment.
Identification Called Out on Metric Prints
On metric prints, color coding, part marking, and packaging sometimes sit in a notes block nobody converts, because it carries no numbers. Those requirements still govern. Reading the whole drawing, not just the dimensioned views, catches them before the first shipment.
Common Problems With Metric Prints for Close Tolerance Ground Parts
Most trouble on metric prints comes from mixing rather than from millimeters.
Mixed Units on Metric Prints
A drawing that gives thickness in millimeters and finish in microinches invites a mistake. So does a note carried over from an older inch revision. Metric prints should be consistent throughout. Any exception belongs marked clearly rather than left for the supplier to find.
Converted Copies of Metric Prints
Once an inch copy exists alongside the original, two documents describe one part. A revision applied to one and not the other produces parts built to a drawing nobody approved. Keeping metric prints as the single master avoids that entirely.
Revision Control on Metric Prints
Each order should name the revision it was placed against. Metric prints revised during a program need the same discipline as any drawing. A reorder against an old revision produces the wrong part while looking correct.
Metric Prints and Customer Expectations
Who issued the metric prints often shapes what else comes with them.
Submission Requirements on Metric Prints
Customers working in millimeters may expect inspection reports, capability data, and approval packages formatted their way. Ask early what form the submission takes. Metric prints from a global platform sometimes carry customer-specific requirements that are not visible on the drawing itself.
Tolerancing Standards Behind Metric Prints
Geometric callouts on metric prints may reference a different standard than an inch drawing would. The symbols largely match, though the governing document can differ. Naming the standard on the drawing removes the guesswork.
Language and Notes on Metric Prints
Notes on metric prints written in another language, or translated unevenly, confuse easily. A short English summary of the critical notes, sent with the drawing, prevents a requirement from being missed without changing the controlling document.
Practical Steps for Metric Prints
A few habits keep metric prints straightforward on both sides.
Agree on Units in Metric Prints Early
On metric prints, settle which unit governs, which gets reported, and how many decimal places appear. That conversation takes minutes at the quote stage. Left until inspection, it can stall a shipment while two correct reports get reconciled.
Check Boundaries Early on Metric Prints
Convert any dimension sitting near a size or thickness limit before the part gets quoted. Metric prints hide those boundaries, since a number in millimeters gives no instinctive sense of whether it fits a process described in inches.
Quoting From Metric Prints for Close Tolerance Ground Parts
A complete package gets metric prints quoted without a round of questions.
What to Send With Metric Prints
Send the drawing at its current revision, the material specification, any hardness requirement, and the thickness steps if the part belongs to a family. Mark which dimensions are critical. Metric prints quoted from a complete package come back faster than ones arriving alone.
Volume and Lot Size on Metric Prints
An accurate estimated annual volume shapes the process plan and the price, whatever unit the drawing uses. Our production grinding programs start above 5,000 pieces per year. Including volume with metric prints lets the supplier recommend the most economical route.
Why Metric Prints Keep Showing Up for Close Tolerance Ground Parts
The share of work arriving on metric prints has grown steadily.
Global Platforms Behind Metric Prints
Vehicle and equipment programs designed for several markets get drawn once, usually in millimeters, and built in multiple countries. A supplier in Michigan can end up quoting a part drawn by an engineering group on another continent. Metric prints are simply the native form of that work.
Suppliers Adapting to Metric Prints
Handling metric prints well is now part of serving automotive and industrial customers rather than a specialty. The measurements, the gauges, and the reporting all accommodate either unit. What matters is agreeing which one governs and holding to it through the program.
Working From Your Close Tolerance Ground Parts Metric Prints
Metric prints describe the same parts as inch drawings, and the only real risk is a conversion nobody agreed to. Keep the metric drawing as the master. Convert limits rather than nominals and tolerances separately, state units on every result, and check dimensions near a process boundary. Northern Industrial Manufacturing Corp. double disk grinds flat parts to 0.025 millimeters total thickness tolerance in an IATF 16949 certified plant in the Detroit area. Send us your drawing in the unit it was designed in, and our team will confirm what can be supplied.
Metric Close Tolerance Ground Parts Manufacturer
Northern Industrial Manufacturing is your premier parts manufacturer for metric close tolerance parts grinding services. With a reputation for the closest tolerances, highest product quality, short lead times, process innovations, and technical prowess – we can meet your close tolerance parts manufacturing needs, while exceeding your expectations and delivering your parts on time and on budget.
If your manufacturing needs calls for precise, dependable close tolerance parts grinding services, the team at Northern Industrial Manufacturing is ready to support you. Call 586.468.2790 or request a quote today to discuss your project and discover how our laser cutting services can support your production goals.
Metric Close Tolerance Ground Parts Manufacturing: 586.468.2790
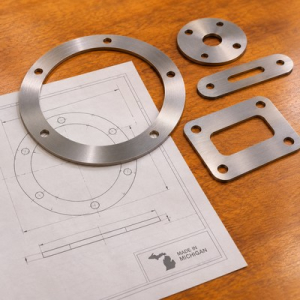
Thank you for visiting our blog where we keep you updated on the latest News and Events in automotive manufacturing!
Please check back often to learn what is going on with Northern Industrial Manufacturing, in the world of precision thrust washers, selective shims, and spacers.
HOURS
Shipping
Monday-Friday: 7:00 am to 3:00 pm
Office
Monday-Friday: 7:00 am to 4:00 pm
CONNECT